
Conveying and Intelligent Sortation: Optimizing Material Flow in a Logistics Center with Storcan
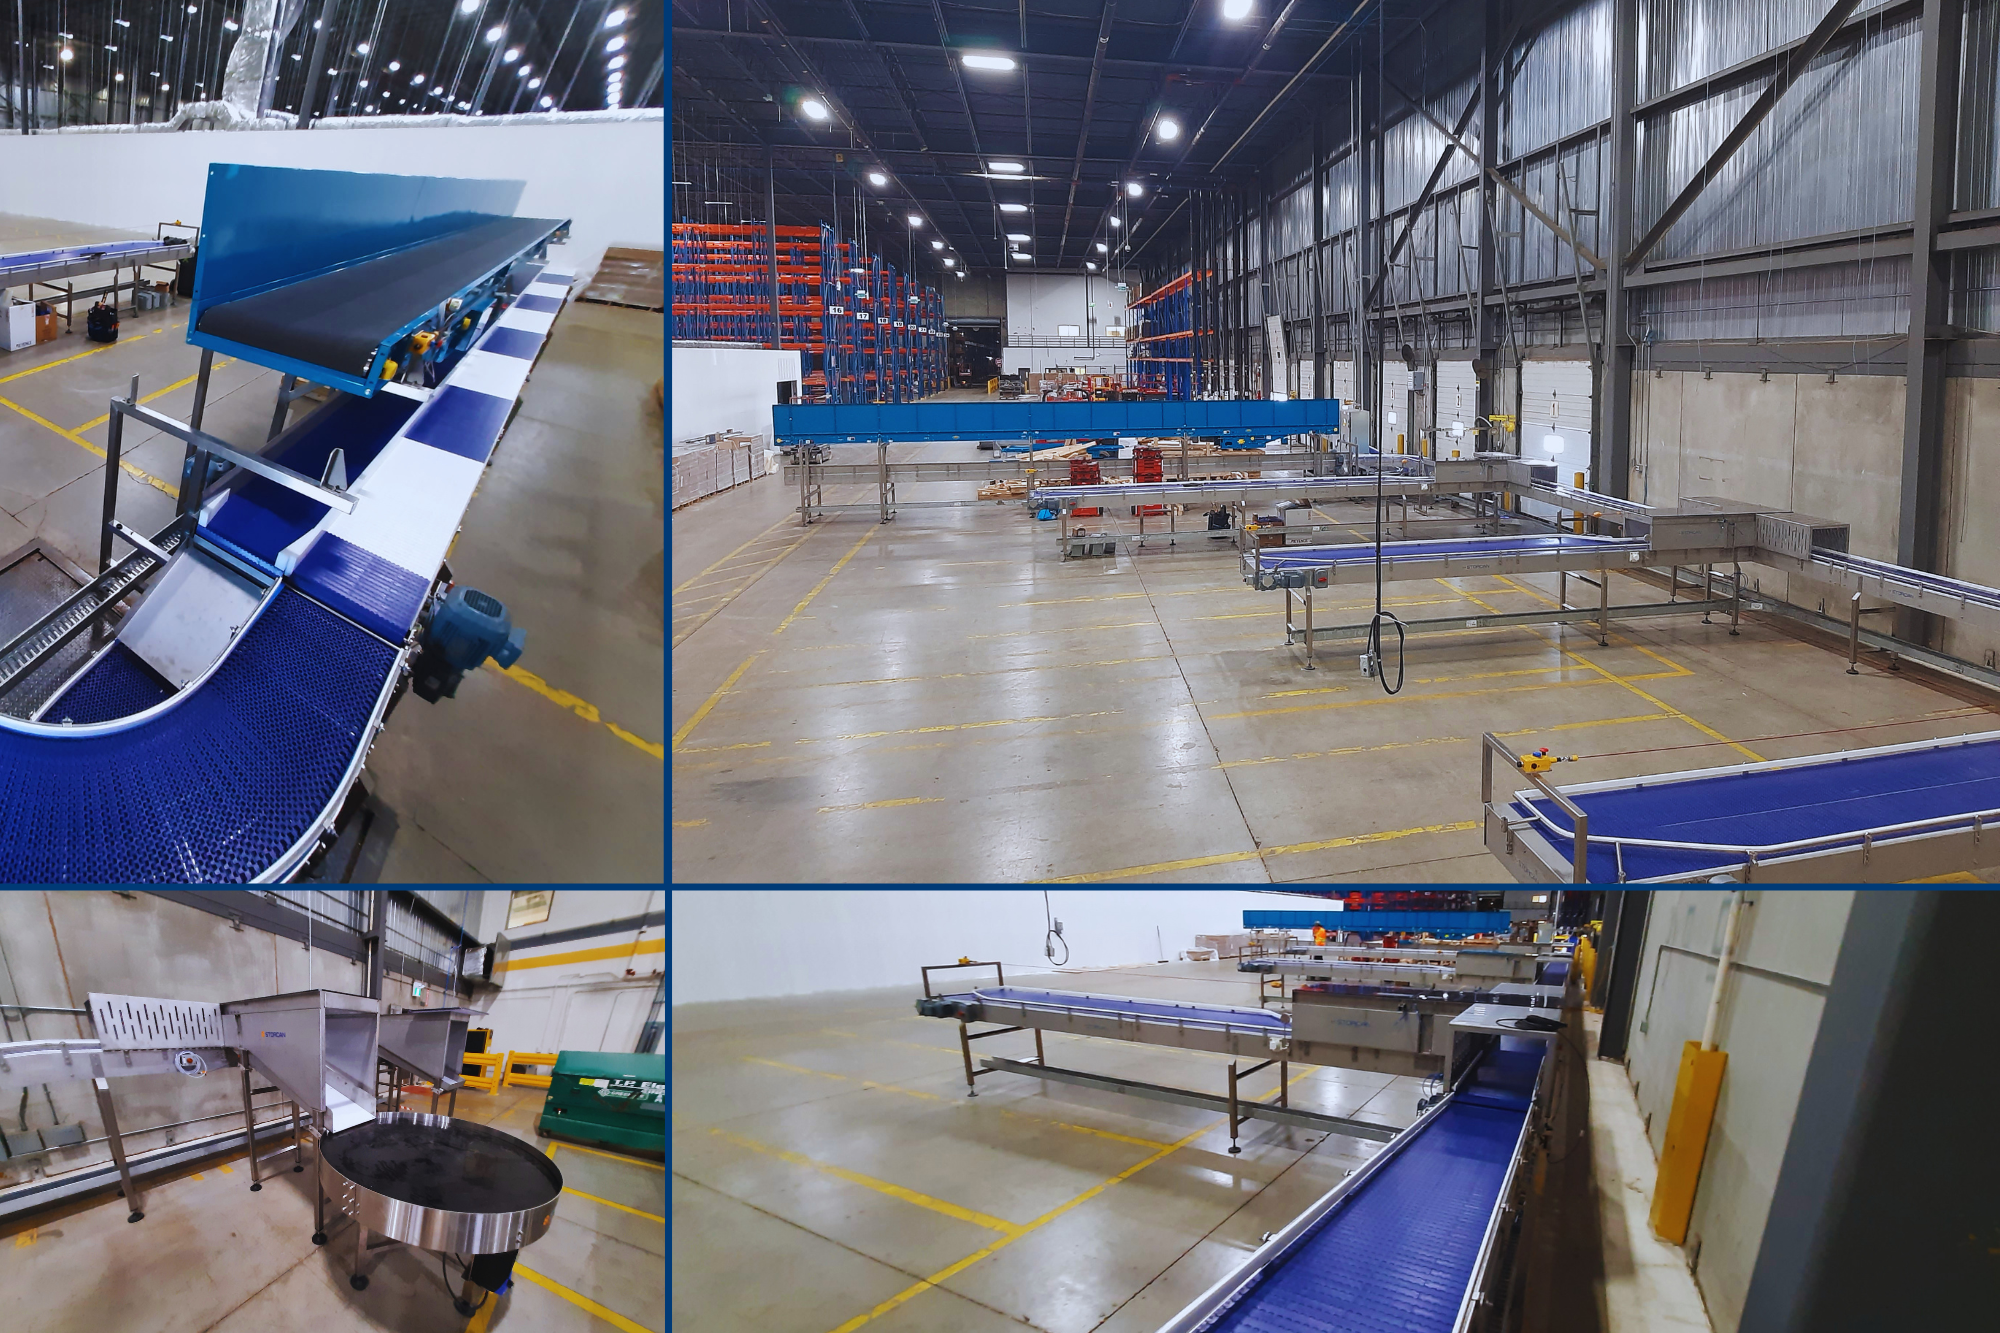
In a logistics center, processing capacity depends as much on material flow as on the equipment used. From receiving onward, each product must reach the right operation while minimizing handling and keeping workstations clear.
Known for its food and beverage expertise, Storcan has also spent years supporting industrial manufacturers and distribution centers with component conveying, carton handling, and the integration of end-of-line and intelligent sortation solutions.
This project illustrates that expertise: designing a custom conveyor system that supports electronic equipment processing and works with the logistics center’s identification and sortation technologies.
Situation and Challenge
Organizing the Processing of Multiple Material Categories
The client is a logistics provider specializing in the design and operation of field service support networks. With facilities across several Canadian provinces, the company serves the national market, with its largest facility located in Toronto.
For this project, the requirement involved processing boxes containing electronic parts, cables, remote controls, and other accessories.
After unpacking, each material category needed to follow a specific path: electronic parts identification and sortation, accessory conveying to manual processing stations, and empty carton removal.
The solution needed to:
- Organize material flow from the unpacking stage;
- Support automated equipment identification and sortation;
- Feed manual workstations consistently;
- Manage product accumulation between operations;
- Remove packaging without congesting work areas.
The challenge was to coordinate these operations within the available space to support throughput and make better use of the facility’s resources.
Storcan Solution
A Custom Solution Supporting Intelligent Sortation
Storcan designed and supplied a solution combining custom-built conveyors with complementary material handling equipment.
The system incorporates conveying, accumulation, and distribution functions tailored to electronic equipment, accessories, and empty cartons, as well as their specific paths through the facility:
- Electronic parts travel to a scanning station and are then directed to processing areas based on their identification. The modular MatTop conveyor system handles their movement and distribution in coordination with the scanning technologies and system controls.
- Accessories follow a dedicated path to manual sorting stations. This arrangement feeds operators while minimizing handling between unpacking and processing. Empty cartons are conveyed separately to a compaction area by a Hytrol belt conveyor, helping keep work areas clear. Its specialized design accommodates long waste removal runs with high side guards to prevent material from falling off.
- Accumulation turntables and recirculation tables complete the system, managing product buffering between operations and supporting continuous processing.
Storcan’s scope included the design and fabrication of custom conveyors, scanning tunnels, encoders, mechanical installation, and startup support. A specialized provider handled the controls, programming, and camera reader supply.
Results
Storcan can work with providers selected by the client or a third party, or take responsibility for overall integration from the design stage of the solution. The scope of responsibility adapts to the project, with the same objective: a cohesive, high-performing, and cost-effective solution.
The solution is designed to support higher throughput by reducing intermediate handling and improving workstation feeding.
The performance drivers are concrete:
- Reduce manual movement by conveying equipment, accessories, and cartons to the appropriate operations;
- Support automated sortation with conveying systems suited to identification technologies;
- Allow operators to focus on product processing through organized workstation feeding;
- Better manage buffering between operations through accumulation functions;
- Keep work areas clear with dedicated packaging removal.
In a logistics environment, these operations repeat throughout the day. How they are organized affects the time spent on each unit, processing capacity, and operating costs. This is where technology selection and integration contribute to profitability.
Expertise Beyond Food and Beverage
Storcan adapts its solutions to the products being handled, space constraints, and operational objectives. This project highlights a capability at the core of our work: understanding how products move through a facility and designing the automation system that effectively connects each processing stage.
With 50 years of manufacturing and integration expertise, Storcan helps companies improve their production lines, end-of-line operations, and logistics flows with one consistent objective: putting technology to work for their profitability.
Looking to optimize conveying, material handling, or sortation in your facility? Contact a Storcan expert to assess your material flow and develop a solution tailored to your operations.